
Treat matching, bias and heat as one design.
An RF power amplifier PCB supports the signal path, bias network and heat-removal structure. Review electrical loss, assembly interfaces and operating conditions together to turn a device-level design into a repeatable board.
An RF power amplifier PCB supports the signal path, bias network and heat-removal structure. Review electrical loss, assembly interfaces and operating conditions together to turn a device-level design into a repeatable board. Use the application-specific review below to identify the information needed for material selection, fabrication and acceptance.
The PCB participates in amplifier behavior
An RF power amplifier board connects an active device to its input, output, bias and thermal environment. Matching networks and transmission-line geometry influence the electrical response. Grounding, supply distribution and the physical assembly can also affect performance, so a device datasheet alone does not define the finished amplifier.
Specify frequency range, input and output power, gain, waveform, duty cycle and operating conditions. If linearity or efficiency is a requirement, define the measurement and the operating point. A saturated-power value and a backed-off modulated measurement answer different questions and should not be compared as if they describe the same test.
Choose a material for RF and thermal needs
A suitable laminate balances electrical loss, dielectric stability, heat transfer, thickness and fabrication requirements. Consider the copper surface and final finish alongside the dielectric data. A thicker or heavier copper construction can change etching and transmission-line geometry, so it should not be selected only from a DC current argument.
The heavy copper and thermal review helps define the conductor and heat-flow assumptions. A laminate thermal-conductivity value is not the complete junction-to-ambient thermal path. Package attachment, vias, spreaders, interface materials and the heatsink can dominate the practical temperature result.
Understand the application interfaces
RF amplifier power and efficiency check
Enter powers at a consistent amplifier boundary. Results are an energy-balance check, not a thermal or linearity simulation.
Drain efficiency = Pout / Pdc; PAE = (Pout − Pin) / Pdc; ideal dissipation = Pdc + Pin − Pout. Specify which supply rails are included. These inputs do not predict junction temperature.
Make the package and cooling interface explicit
Provide the device land pattern, exposed-pad requirements and the manufacturer’s assembly guidance. Define any via filling or capping, solder void acceptance if required, cavity or coin interface, fastening and thermal-contact requirements. A mechanical section drawing is often necessary where the device transfers heat to a chassis or a spreader.
Review soldering access, thermal mass and the inspection method before fabrication. If a package or heat spreader changes, check the assembly process as well as the thermal model. Connect the fabrication package to the RF assembly scope so that the board and assembly assumptions remain consistent.
Compare efficiency metrics correctly
Drain efficiency uses RF output power divided by DC power at the defined boundary. Power-added efficiency subtracts RF input power from RF output power before dividing by DC power. The distinction matters when comparing devices or operating points. Use consistent units and clearly identify which bias rails and auxiliary circuits are included.
The tool below calculates both metrics and a simplified energy-balance dissipation from user-entered powers. It does not predict temperature, stability, linearity or reliability. Negative dissipation or efficiency beyond a physically consistent boundary indicates that the input values or measurement boundaries need review. Confirm the cooling requirement with a thermal model and representative measurements.
Application-to-manufacturing review
| Area | Define for the application | Confirm before release |
|---|---|---|
| RF requirement | Band, power, gain and waveform | Operating point and measurement boundary |
| Bias | Supply rails, current and sequencing | Copper distribution and device guidance |
| Thermal interface | Package, vias, spreader and heatsink | Assembly contact and temperature limits |
| Validation | Efficiency, gain and relevant linearity tests | Fixture, load, cooling and pass criteria |
Connect these requirements to the Heavy Copper & Thermal PCB Engineering workflow. The approved stackup, drawing and order-specific acceptance plan define the build.
Build the acceptance plan around the application
Decide what the bare board must demonstrate and what belongs to the assembled product. Continuity testing, an impedance coupon, a calibrated RF network measurement and an installed-system test are different forms of evidence. None should silently stand in for another. Identify the required report, coverage, limits and review responsibility before the quotation is accepted.
Record the test configuration alongside the result: board revision, material construction, fixture, calibration, firmware or device settings, temperature and the relevant operating point. When comparing prototypes, keep these conditions consistent or explain the difference. A changed connector, cable or reference plane can make an apparent board improvement difficult to interpret.
For production, agree how first-article findings become controlled manufacturing requirements. Identify which dimensions and material choices are critical, what may be adjusted by engineering, and which changes require renewed validation. A repeat order should reference the approved revision and test plan rather than rely on a previous email description.
Visit quality and test evidence for supplier qualification and reporting questions. Where a customer program requires certificates or sector-specific approval, request the actual documents and applicable scope. An application example is not a product certification or a substitute for the customer’s acceptance process.
Prepare a quotation that engineering can review
A useful RF PCB quotation starts with a controlled design package. Send Gerber or an agreed manufacturing format, NC drill data, a dimensioned outline, the board revision and a stackup drawing. Add quantity, delivery destination and the requested schedule. If some details are still open, mark them explicitly instead of letting a drawing, an email and a file name imply different requirements.
Separate mandatory requirements from preferences. A specified laminate, a customer-approved alternative and a request for a recommendation are three different purchasing instructions. State whether the supplier may propose changes to dielectric thickness, line geometry, panelization or finish, and who approves those changes. Changes that affect RF behavior should return to the design owner before release.
What affects the price?
Board area and panel utilization, quantity, material availability, stackup complexity, drilling and plating, special mechanical features, inspection and test all influence cost. Tight tolerances can also change the achievable yield and process route. An online estimate cannot account for every interaction in an unusual construction.
Use the panel and material cost tool to explore the assumptions it exposes, then request a reviewed quotation. Confirm tooling or setup charges, engineering changes, shipping, taxes and the included report package in the commercial offer.
What affects delivery?
Material stock, engineering clarification, special tooling, lamination cycles and the agreed inspection plan can affect the schedule. Assembly adds component procurement, stencil preparation, programming and fixture readiness. The requested date is a planning input until the supplier confirms the complete order scope.
The website’s response-time target describes enquiry handling. It is not a guarantee that a complex RF build can be priced, fabricated or delivered within the same period. Ask the team to identify the critical dependencies for your project.
From review to repeatable production
Agree the build
Engineering reviews material, geometry, mechanical features and test requirements. Open questions and proposed changes are documented. The approved drawing and stackup become the manufacturing baseline.
Verify the first build
Define which records are needed for the prototype: electrical test, impedance, dimensional inspection, cross-sections or an agreed RF measurement. Evaluate the evidence against the relevant acceptance criteria.
Control later changes
Keep revision, material substitutions, process changes and test updates traceable. A successful prototype is the starting point for production control, not permission to change the construction silently.
For a performance issue, retain the board revision, lot reference, measurement setup and operating conditions. Comparing repeatable measurements is more useful than comparing screenshots taken with different fixtures or calibration. Define the investigation and disposition with the supplier using the actual order requirements.
Prepare your RF power amplifier PCB enquiry
Select what is ready. This checklist runs locally and does not upload files or place an order.
Real manufacturing and laboratory context
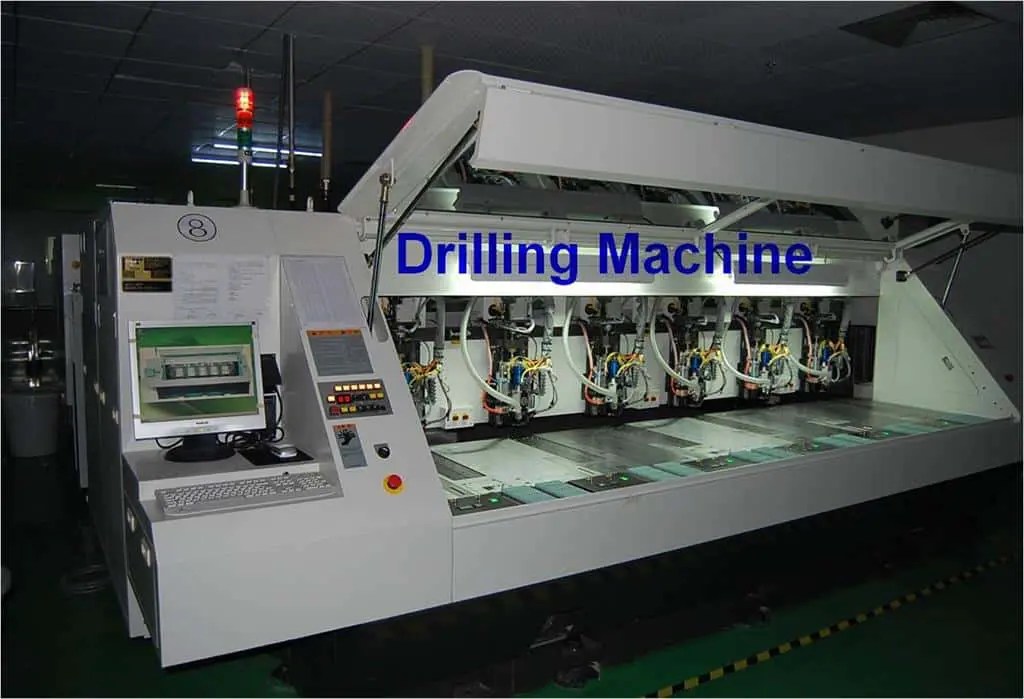
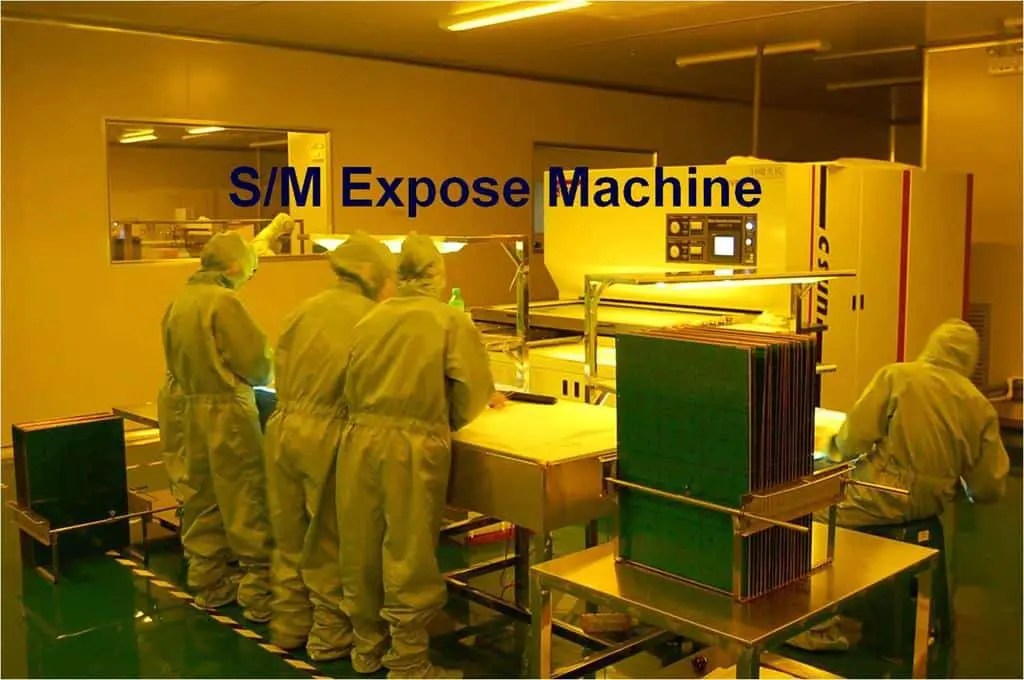
These photographs are from the shared RFPCB / PCBSync facility archive. They show manufacturing and laboratory areas, not a claim that a pictured item is a certified RF power amplifier PCB product. Review the actual process and report requirements with the team.
RF Power Amplifier PCB Manufacturing: common questions
Are drain efficiency and PAE the same?
No. PAE subtracts the RF input power; drain efficiency does not. Both depend on the stated power boundary.
Does thicker copper guarantee a cooler amplifier?
No. The complete thermal path, current distribution and operating conditions must be evaluated.
Can the calculator predict junction temperature?
No. It estimates power relationships from inputs. Thermal resistance, spreading and cooling are not modeled.
Related application decisions
Base Station RF PCB Manufacturing
A base station PCB can combine RF distribution, amplification, power and control. Define the board function, operating band and environmental requirements before choosing a material or a production process.
Satcom & Aerospace RF PCB Manufacturing
Satellite communication and aerospace RF boards span ground terminals, airborne equipment and spacecraft hardware. These environments have different requirements; the manufacturing and qualification scope must identify the actual end use.
5G & mmWave PCB Manufacturing
A 5G or millimeter-wave PCB brings RF interconnects, antenna structures and digital control into a tightly coupled design. Select the stackup around the actual operating band and bandwidth rather than the 5G label alone.
Technical references and scope
Use current component and material documentation together with the approved design. The sources below provide engineering context; the specific product and manufacturing acceptance requirements remain project-dependent.
- Analog Devices: power-added efficiency
- Rogers thermal solutions
- RFPCB material selection and engineering tools
- Manufacturing capability review
Engineering guide updated September 2026. Diagrams are conceptual and not production drawings. Calculations are estimates under the stated assumptions.
Bring the application requirements into the quote.
Send the operating band, board revision, stackup, quantity and acceptance needs. The team can identify missing information and review the proposed manufacturing scope.
Related engineering decisions
Ready for a quotation?
Send your requirements for a material, stackup and manufacturing review. Price and schedule are confirmed for your project.